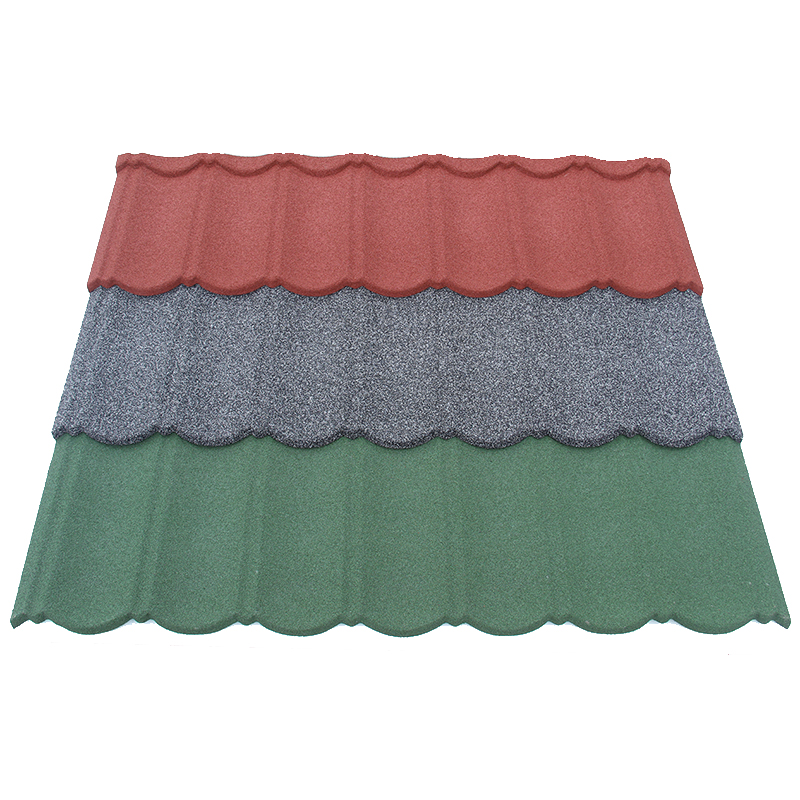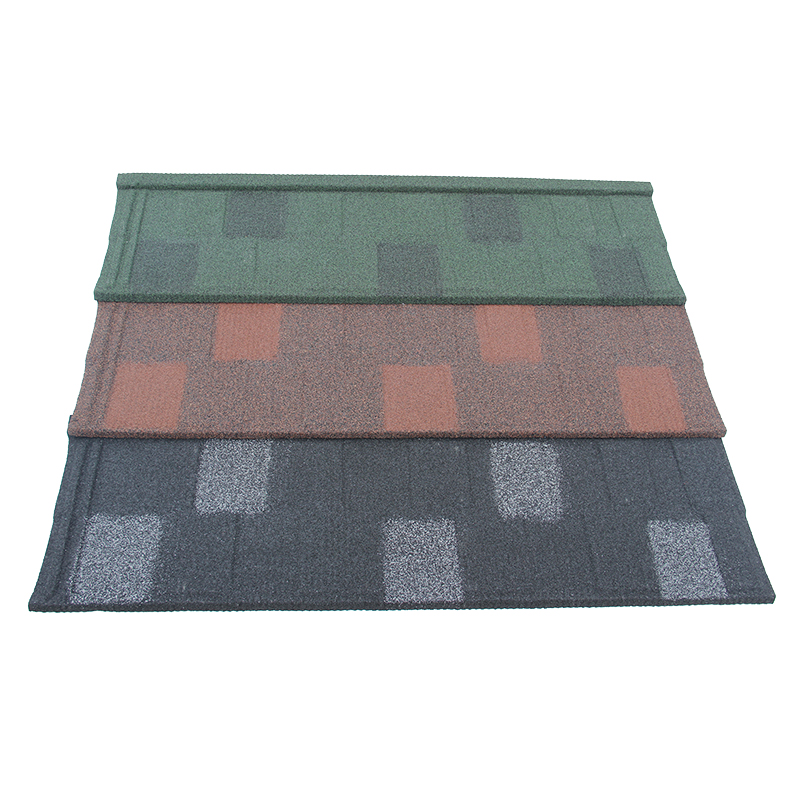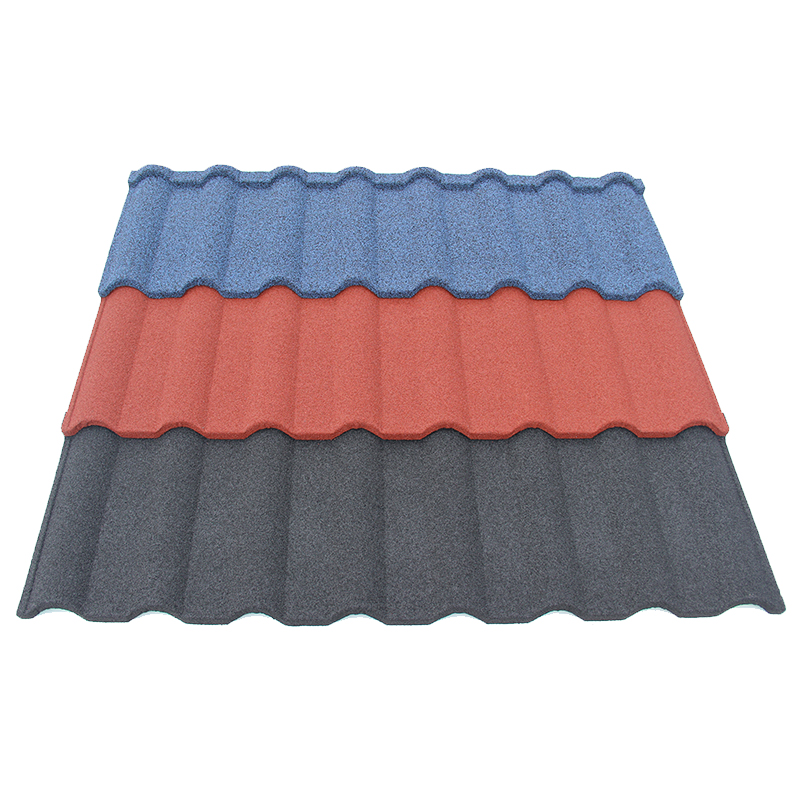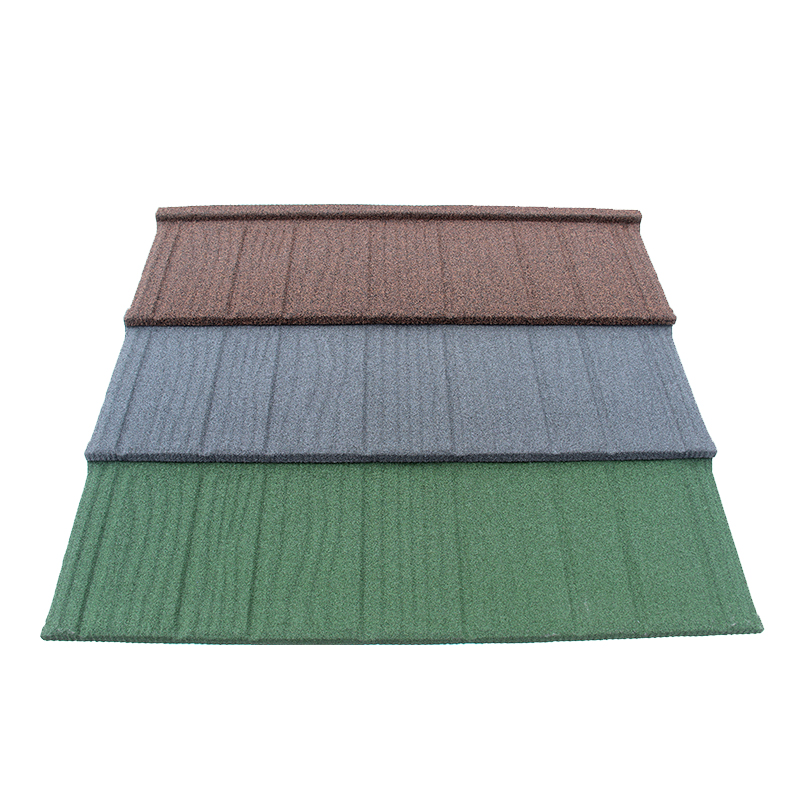

Stone coated metal roofing production capacity should be demonstrated as accepted output available for your order. Ask the supplier to connect its claim to operating records, product mix, material availability, and existing commitments. Machine speed or annual output alone cannot establish a dependable delivery schedule.
Can the supplier complete your specified tiles, accessories, and packing within the agreed period? That is the practical wholesale question. The answer needs a clear unit, defined operating conditions, and a realistic explanation of constraints. A larger factory number does not automatically mean more available capacity.
This guide explains how to evaluate that evidence before placing a bulk order. It includes a transparent planning example, clearly separated from supplier performance claims. Use the method with verified records from the factory you are considering.
Define What the Capacity Claim Actually Measures
Distinguish machine output from accepted roofing output
Ask whether the quoted figure represents formed blanks, coated tiles, inspected products, or packed goods. Those are different points in production. A forming machine may operate faster than later coating or packing stages. Capacity at one stage therefore cannot represent the entire order without checking downstream processes.
Identify the unit and product basis. Suppliers may report pieces per hour, square meters per day, or annual output across multiple products. Request the profile, effective coverage, and operating assumptions behind the figure. Mixed units should be converted only after the relevant product definitions are confirmed.
Separate theoretical maximum output from demonstrated performance. Theoretical figures may assume uninterrupted operation and a favorable product configuration. Actual records should show what happened under normal working conditions. Ask which losses, changeovers, and quality requirements are included before using the number for planning.
Equipment information can clarify the process boundary. Yusheng’s production line page lists forming, coating, curing, and stacking stages. It also leaves throughput dependent on the configured line. That illustrates why buyers should request configuration-specific evidence instead of borrowing a generic equipment rate.
Make product coverage and order scope explicit
Request the effective coverage assigned to each proposed tile. Keep that value separate from nominal sheet dimensions and the roof’s total material requirement. Where different profiles are mixed, calculate their quantities independently. The product basis must remain consistent between quotation, production planning, and shipment documents.
For example, a Bond Tile order should use the supplier’s confirmed specification for that product. Do not apply another profile’s coverage or packing assumptions. Accessories also need separate quantities and production checks. Field tile output alone may leave the shipment incomplete.
Clarify whether the capacity claim includes all products made at the site. A factory may report combined output from roofing tiles and other building products. Ask which equipment and shifts would serve your order. Company-wide totals can provide context, but order planning requires the relevant production resources.
Supplier introductions are a starting point for this discussion. The JCROOF company page provides background for buyers evaluating a roofing supply relationship. Ask for current production evidence and an order-specific plan. Do not substitute a general company description for confirmed available production time.
Check the Evidence Behind Sustainable Output
Review operating records and the bottleneck
Request recent records covering representative production conditions. Identify the product mix, scheduled hours, actual operating time, and accepted quantities. Ask how rejected goods and rework are recorded. Sustainable capacity should reflect usable output, rather than counting every piece that briefly passes through a machine.
Follow the product through each stage. Compare forming output with coating, curing, inspection, and packing records. The slowest relevant stage may limit completed order output. Ask how the supplier identifies that constraint. Check how its production schedule responds when the product mix changes.
Review changeovers for profiles and colors. Ask what must be cleaned, adjusted, checked, or approved before the next item starts. A mixed order can require more preparation than a long run of one product. The schedule should show these transitions rather than assume the maximum continuous rate applies throughout.
Observe whether the proposed resources are operational. Installed equipment may be idle, under repair, or assigned to another product. Request maintenance information where it affects the plan. Additional shifts also need staffing and supervision, so a theoretical overtime option should not be treated as confirmed output.
Confirm materials and quality capacity
Ask which critical materials are available for your specification. Confirm the proposed steel, finish materials, accessories, and packaging rather than general warehouse stock. Material quantities need to relate to your product and order. An unrelated stockpile cannot resolve a shortage for a customized color or specific substrate.
Check procurement dependencies where materials still need purchasing. Ask when specifications must be finalized and who confirms availability. Identify what happens if a material arrives late or fails incoming checks. The supplier should describe the approved response without assuming that an alternative material is automatically acceptable.
Review quality staffing and inspection availability. Higher output can increase the workload for checking, documentation, and handling rejected products. Ask whether those functions can support the proposed schedule. Production capacity that depends on bypassing agreed checks is not suitable capacity for your purchasing requirements.
SGS quality audits evaluate manufacturing processes and quality systems against defined needs. Such assessment can support investigation of operational uncertainties. Specify the relevant capacity questions and records before commissioning the work. A general audit title alone does not establish your order’s available production slot.
| Capacity question | Useful evidence | Common misunderstanding |
|---|---|---|
| What output is measured? | Defined product and production stage | Counting blanks as packed goods |
| What limits completion? | Stage-level operating records | Using only forming speed |
| What output is accepted? | Rejection and rework records | Counting every produced piece |
| What time is available? | Schedule and existing commitments | Treating total output as free capacity |
| What materials are allocated? | Order-specific material confirmation | Assuming general stock is suitable |
| Are accessories ready? | Component supply and packing plan | Treating field tiles as a complete shipment |
Translate Capacity into an Order Completion Plan
Use a transparent calculation with verified inputs
Build the planning calculation from confirmed production data. Start with demonstrated accepted output for the relevant product and operating conditions. Multiply by the production time actually allocated to your order. Then identify commitments or constraints not already included in that allocation, avoiding double counting.
If you start from a theoretical production rate, explicitly account for downtime, changeovers, and acceptance yield. If you use actual accepted output records, check which losses they already contain. Applying the same deductions again would understate capacity. Mixing both approaches without explanation creates a misleadingly precise result.
Consider this hypothetical calculation, unrelated to any supplier’s actual performance. Assume demonstrated accepted output is 600 tiles per operating day under the relevant conditions. If ten comparable days are allocated, planned output is 6,000 accepted tiles. Both input values would require verification before use in purchasing.
Now assume another confirmed commitment consumes 1,500 tiles of that same allocated output. The remaining quantity would be 4,500 tiles, provided the allocation previously included both orders. Do not subtract that commitment again if the ten days were reserved exclusively for your order. The schedule definition determines the calculation.
Plan completion across the full item list
Create a timeline for every required profile, color, and accessory. Record the production sequence, inspection readiness, packing completion, and expected dispatch availability. Distinguish the supplier’s forecast from confirmed milestones. A single date without its dependencies gives buyers little opportunity to detect an emerging delay.
Ask for evidence of the allocated production slot. The supplier can conceal confidential customer identities while showing relevant commitments and resource availability. Confirm who authorizes the schedule and when it will be reviewed. A salesperson’s estimate should connect to the production plan used by the manufacturing team.
Include approval dependencies controlled by the buyer. Delayed artwork, samples, or technical decisions can affect production readiness. State when each approval is required and what changes if it arrives later. This creates a shared schedule rather than placing every uncertainty inside one unsupported delivery promise.
Separate production completion from shipment readiness. Inspection, packing corrections, document preparation, and transport coordination may occur afterward. Request milestones for those activities without assuming universal durations. Buyers need the complete readiness sequence to coordinate warehouse demand and communicate realistically with downstream customers.
Verify the Plan Through Milestones and Repeat Orders
Monitor signals that show progress
Agree which updates will demonstrate production progress. Useful evidence may include identified material receipts, completed batch records, inspection results, and packing status. Photos should show the relevant item and date context where practical. A warehouse picture without product identification cannot establish progress for your particular order.
Review actual progress against the item-level schedule. Ask about differences early, before unfinished components prevent shipment release. Require the supplier to explain the affected quantity and recovery options. A revised date is more useful when its reason and dependencies are clear to everyone managing the order.
Address recovery without weakening the specification. Additional shifts, alternative sequencing, or split deliveries may be possible, depending on agreement. Material substitutions and outsourced production need separate approval where required. The recovery discussion should preserve traceability and agreed quality controls throughout any revised plan.
For a first order, choose milestones that test the claimed capability. Inspect representative products and evaluate the completeness of records and packing. Track whether accepted output matches the production explanation. Use the result to improve planning inputs before committing to a larger or more complex order.
Reassess available capacity as conditions change
Available capacity can change with demand, maintenance, materials, staffing, and product mix. Request current confirmation for each significant order rather than reusing an old annual figure. A supplier’s earlier successful shipment provides useful history. It does not automatically reserve the same resources for your next purchase.
For replenishment programs, share a realistic forecast and distinguish it from confirmed purchase quantities. Ask how the supplier handles changes in demand and scheduling. Define when a forecast becomes an approved production commitment. This helps both parties avoid treating tentative expectations as guaranteed factory allocation.
Review delivery performance using consistent definitions. Compare the agreed milestone with actual completion of accepted goods, rather than unrelated production events. Include the reasons for delay and corrective responses. Those records can show whether the supplier’s planning approach becomes more dependable across repeat orders.
Wholesale capacity is the ability to deliver your defined order under controlled conditions. Require a clear measurement basis, representative operating evidence, and a schedule tied to real resources. Check the full item list and monitor meaningful milestones. Those connections matter more than the largest number in a supplier presentation.