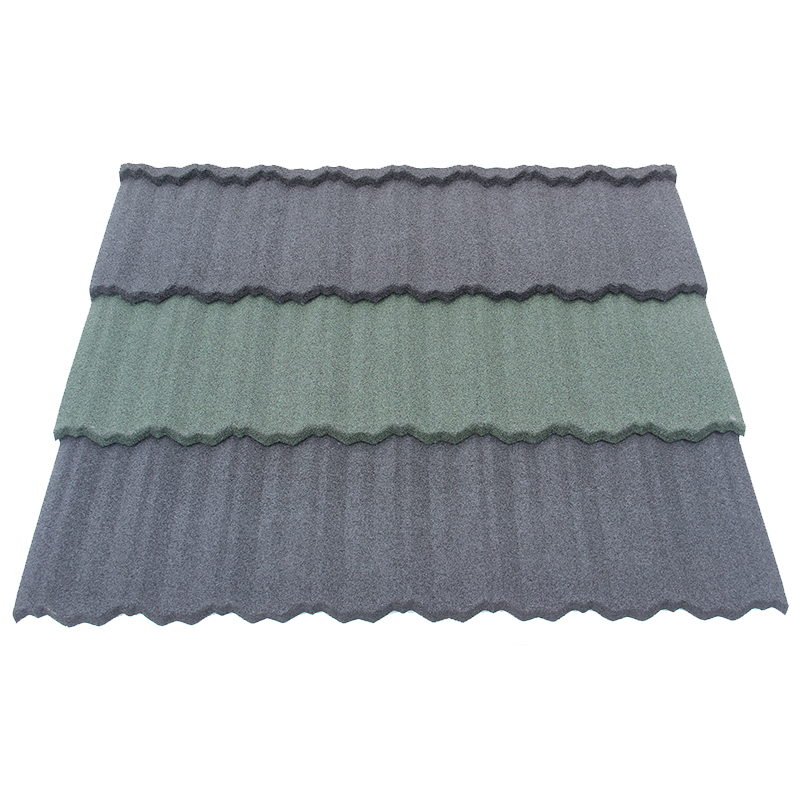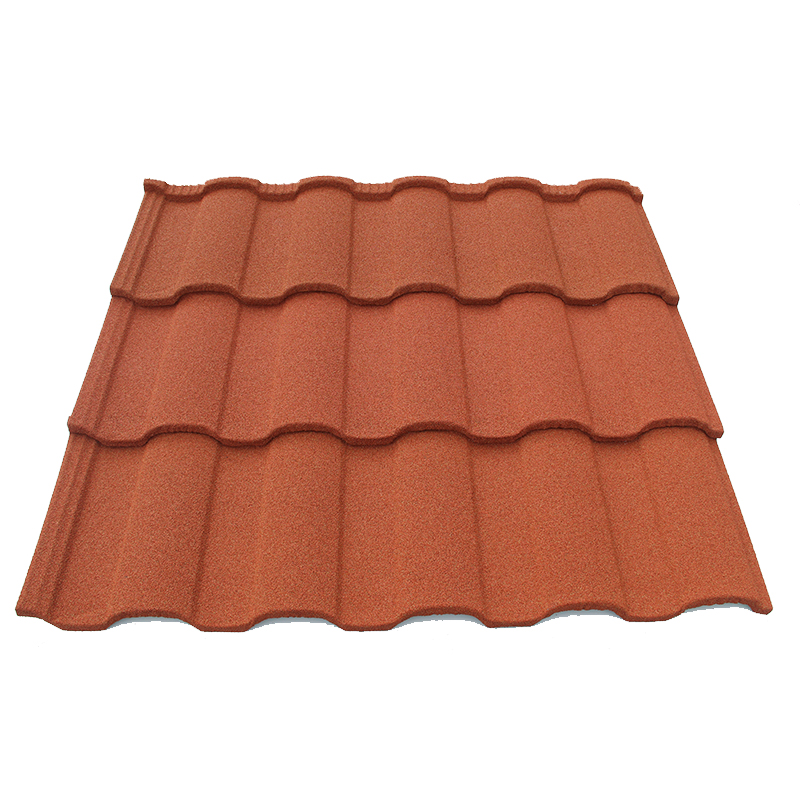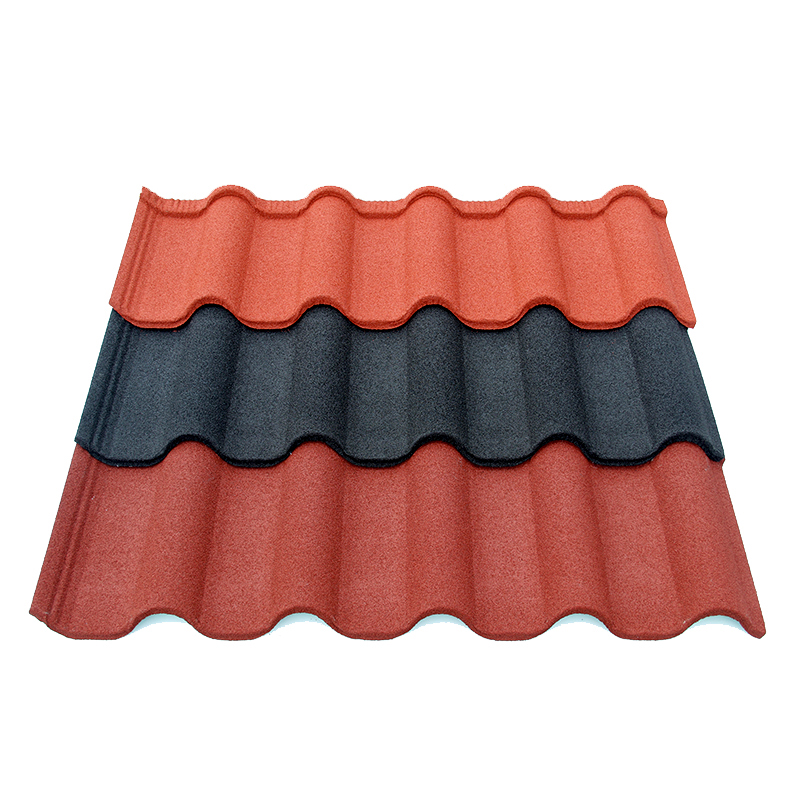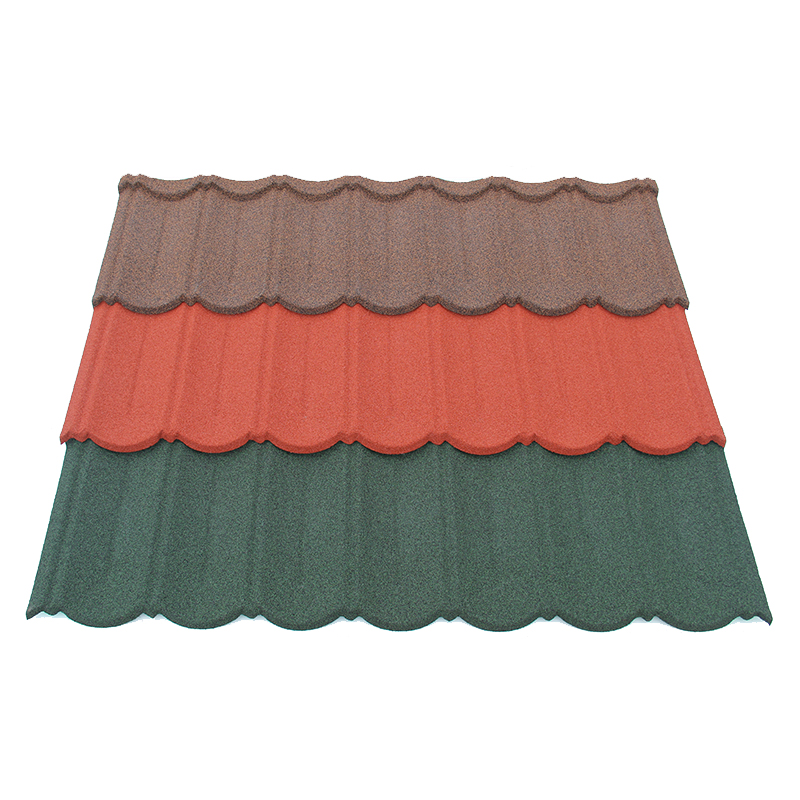

Stone coated roofing factory quality control should connect agreed requirements with named responsibilities, recorded checks, and controlled release decisions. Ask how the factory detects problems, contains affected products, and verifies corrections. A list of testing equipment cannot answer those questions alone.
For overseas buyers, the useful outcome is a clear understanding of how the proposed order will be controlled. You need to know what happens during normal production and when results are unacceptable. Both situations matter when assessing a stone coated metal roofing manufacturer.
This guide focuses on management capability rather than individual test procedures. Use it to review the factory’s actual arrangements against your purchasing needs. Keep conclusions limited to the products, activities, and records examined.
Start with responsibilities and agreed requirements
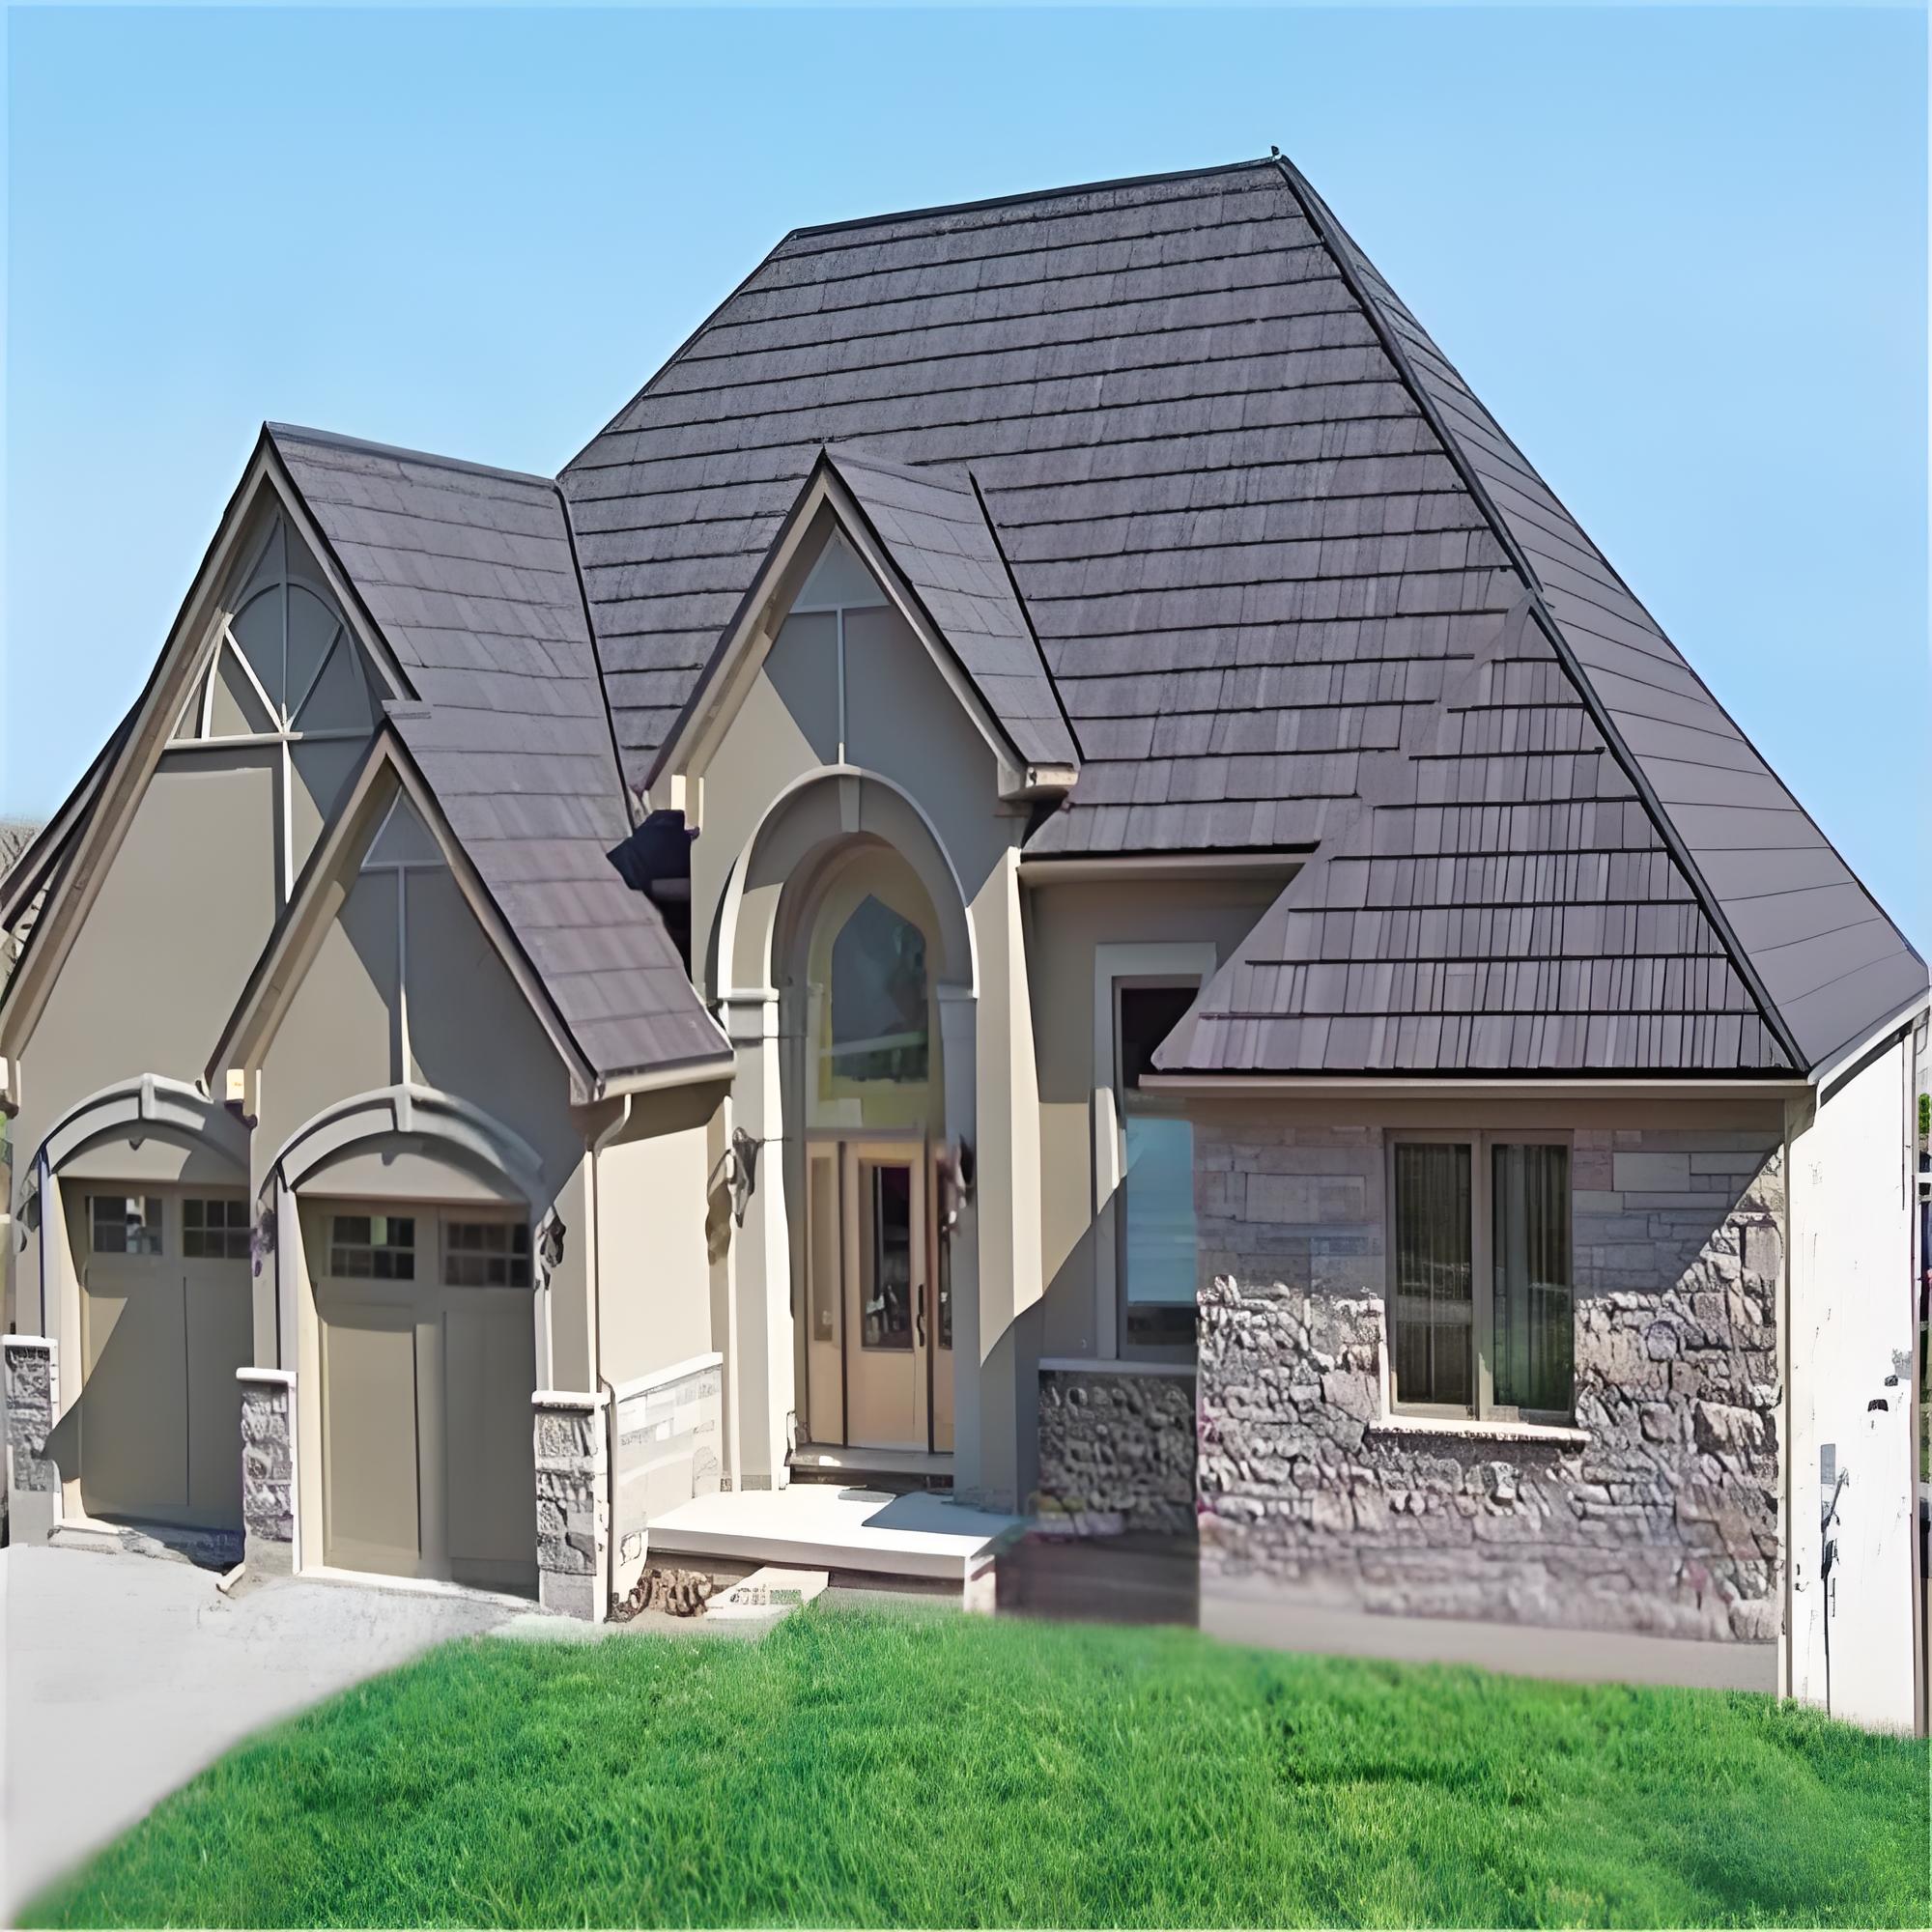
Quality control begins with a usable definition of what the factory must supply. Connect that definition to the people making production and acceptance decisions. Otherwise, different departments may work from different assumptions while using the same product name.
Connect the purchase specification to the control plan
Identify the proposed profile, material description, finish, accessories, packaging, and relevant document revisions. Separate confirmed requirements from details still under discussion. A quotation that says only stone coated roofing leaves too much for later interpretation.
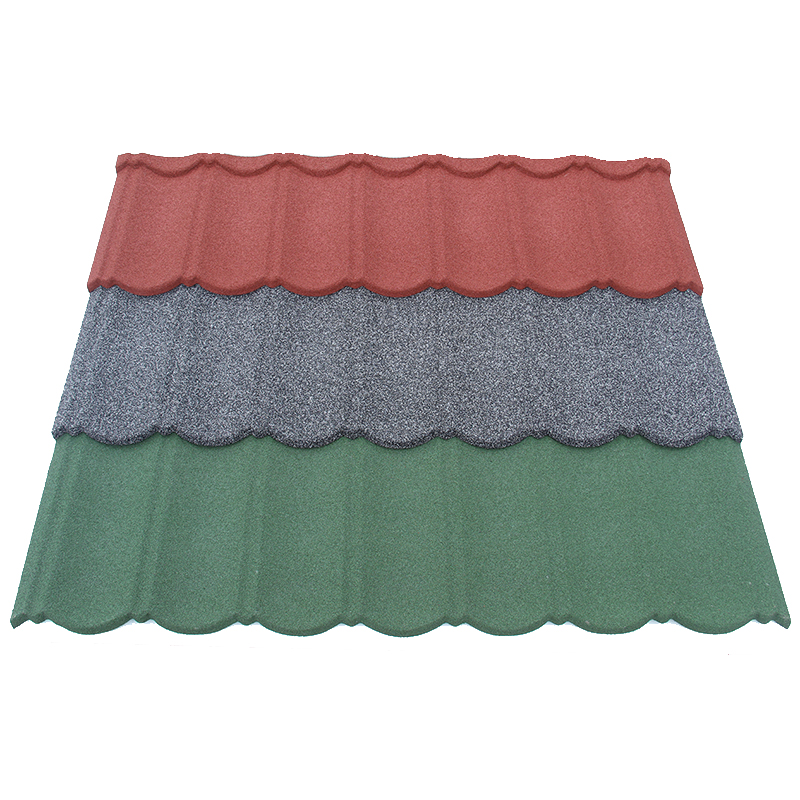
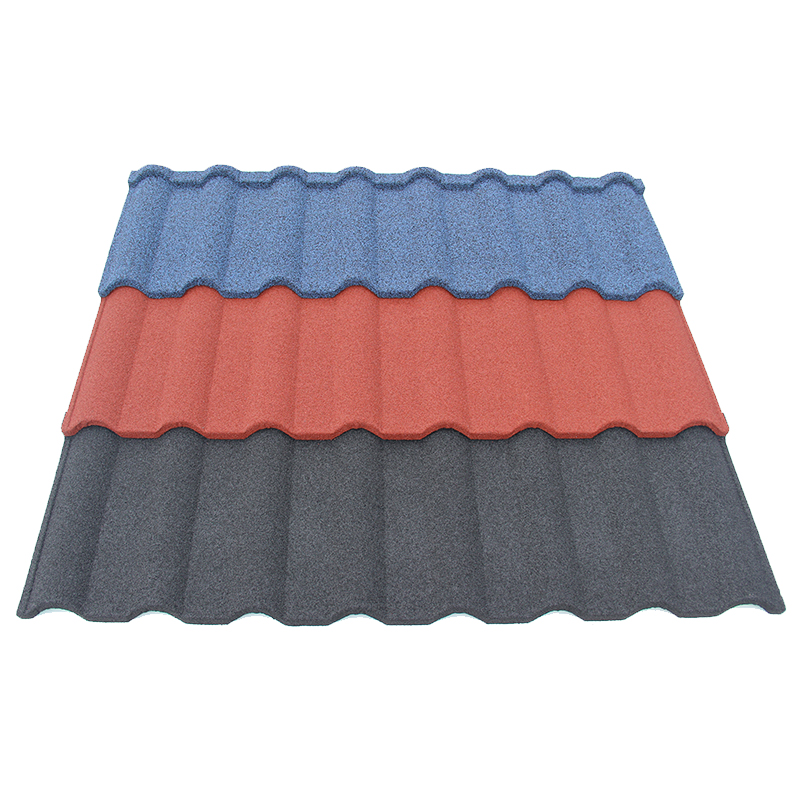
For a Bond Tile inquiry, ask which controlled specification describes the offered version. The profile name is a starting point for identification. It does not establish every material or performance characteristic.
Ask the factory to explain its control plan using your proposed product. Which characteristics are checked, at what stage, and against which acceptance criteria? Request the associated method references and responsibility assignments where relevant.
The SGS quality-audit overview describes factory assessments as reviews of manufacturing processes and quality systems. That supports looking beyond a finished-product demonstration. It does not establish that any particular supplier has passed such an assessment.
Use a current roofing specification checklist to organize the purchasing inputs. Then verify how those inputs reach production and inspection. A complete checklist is useful only when the accepted requirements become operational instructions.
Identify who can stop work and approve release
Ask who owns incoming checks, production checks, final inspection, and release. Confirm how these people communicate when results conflict. Job titles alone do not show whether the responsibilities are understood during ordinary work.
Discuss a recent anonymized example involving an unacceptable result. Who identified the issue, who placed the material on hold, and who decided the next step? Request records that connect those actions without exposing another customer’s confidential information.
For a supplier such as JCROOF, use the company introduction to identify the appropriate quality and production contacts. Ask them to explain the arrangements applicable to your inquiry. Do not infer an internal approval structure from a general company description.
Clarify how commercial pressure is handled when release conditions remain unmet. Ask who can authorize an exception and what buyer approval is required. Any proposed deviation should be explicit before affected goods are accepted.
Follow controls through ordinary production
Review evidence from routine work rather than relying only on a prepared demonstration. Select records relevant to the proposed product and site. Explain why each record matters to the purchasing decision you need to make.
Review incoming and in-process records
Ask how incoming materials are identified, checked, and assigned an acceptance status. Compare the documented material description with the purchase specification. A supplier document and a factory receiving record should have an understandable relationship.
Follow the relevant production activities through their actual sequence. Ask where checks occur and what happens between them. Avoid assuming every factory uses identical equipment, process stages, or terminology.
Compare recorded results with the applicable criteria and document revision. Look for dates, product references, responsible personnel, and understandable decisions. A page filled with numbers is less useful when nobody can explain what was measured.
Ask how changes to materials, settings, methods, or external providers are reviewed. Determine which changes require additional checks or buyer agreement. An accepted sample should not become permission for undocumented changes during later production.
Where outside activities are involved, review the manufacturer outsourcing questions. Focus on how requirements and results pass between organizations. Outsourcing changes the control interfaces that need examination; it does not automatically establish poor quality.
Check equipment, methods, and record credibility
Ask which equipment is suitable for the characteristics being checked. Request the relevant equipment identification and control records. The useful question is whether a recorded measurement can support the stated decision.
Review how inspection methods are communicated and how personnel demonstrate their understanding. Ask what happens when equipment is unavailable or its status is uncertain. Record any effect on products accepted using the affected method.
Distinguish final acceptance sampling from ongoing process control. NIST’s explanation of acceptance sampling describes its purpose as deciding whether a lot is acceptable. A single lot decision does not establish consistent control over future production.
Ask a qualified reviewer to assess whether the proposed sampling arrangements suit your requirements. Do not choose sample sizes or acceptance limits from an unrelated order. Document the agreed basis before interpreting the inspection results.
If records look unusually uniform, ask how results are generated and reviewed. Seek explanations through normal evidence checks rather than making immediate accusations. Separate missing information, unclear practices, and demonstrated contradictions in your findings.
Examine what happens when results are unacceptable
The handling of failures can reveal more than a carefully selected passing record. Review an example from detection through its final disposition. Keep the original finding visible when evaluating the subsequent response.
Separate hold, rework, and release decisions
Ask how suspect material is identified and prevented from accidental use or shipment. Examine the relationship between physical identification and recorded status. A hold instruction is ineffective if warehouse staff cannot identify the affected stock.
Clarify the options used for rejected material and who approves each option. Rework, rejection, and acceptance under an agreed exception are different decisions. Their records should make those differences understandable to later reviewers.
If rework is proposed, ask what instructions apply and how the result is checked again. Confirm that the original failed result remains identifiable. Repeating a check without explaining the intervening action leaves an important gap.
Ask how affected quantities and related batches are considered. The review should explain why the chosen boundary is appropriate. Do not assume that isolating the visibly defective pieces addresses every potentially related product.
Connect these questions with your pre-shipment inspection scope. Final inspection can examine relevant shipment conditions. It should not silently replace unresolved factory controls or erase a known production exception.
Look for evidence that corrective actions work
A correction addresses the immediate problem; preventing recurrence requires understanding why it happened. Ask the factory to explain that distinction through an actual example. Avoid accepting a generic promise of more careful work as sufficient evidence.
Review the identified cause, assigned action, responsible person, and follow-up result. Ask what changed in the relevant work instructions or controls. The explanation should connect the action to the original failure.
Look for later records that test whether the change remained effective. A completed action form alone cannot demonstrate this. If follow-up evidence is unavailable, record the condition as open rather than describing the issue as resolved.
Ask how relevant lessons reach other shifts, product versions, or external providers. Keep the required coverage proportionate to the demonstrated cause. Avoid expanding a conclusion beyond the activities actually reviewed.
Turn the factory review into a purchasing decision
Organize the findings around the requirements your team must satisfy. State the evidence, its limits, and the outstanding decisions together. This makes the review useful for colleagues who did not attend the factory discussion.
Use a focused quality-management review table
Use the following table as a starting structure rather than a universal approval score. Add product-specific requirements with appropriate technical input. Retain clear references so the supporting evidence can be found again.
| Review area | Evidence to examine | Question before approval |
|---|---|---|
| Requirements | Current specification and control plan | Are the same requirements used across departments? |
| Responsibilities | Assigned checks and release authority | Who acts when a result is unacceptable? |
| Incoming materials | Identification and acceptance records | Is material status connected to production use? |
| Production checks | Methods, results, and criteria | Can the factory explain the recorded decisions? |
| Equipment | Relevant identification and control status | Are measurements suitable for their intended decisions? |
| Rejected material | Hold and disposition records | Can suspect stock be prevented from shipment? |
| Corrective action | Cause, action, and effectiveness review | Is recurrence addressed with supporting evidence? |
| Release | Final authorization and exceptions | Are all required conditions closed or explicitly agreed? |
Keep approval conditions connected to follow-up
Separate satisfactory findings from conditions requiring further evidence. Assign each condition to a responsible person and an agreed review point. Avoid a general approved label that hides unresolved requirements.
Consider whether an independent assessment is appropriate for important gaps. Define its product, site, and process scope before commissioning work. A broad certificate or unrelated audit summary may not answer the specific concern.
Keep the final decision with the accepted specification and purchasing record. Revisit affected conclusions when the product, factory arrangement, or agreed requirements change. Quality control is useful when its decisions remain connected to the order being supplied.